Introduction: Background of the Sublimation Industry
Sublimation phone cases, with their core advantages—personalized customization, high color fidelity, and wear-resistant durability—are seeing steadily rising demand across cross-border e-commerce platforms, offline custom shops, and corporate gift orders. Blank consumables (unfinished blanks), as the essential substrate in sublimation phone case production, directly determine the finished product’s color performance, abrasion resistance, and service life; they are thus a critical link influencing the competitiveness of end products.
When seeking suppliers or manufacturers for sublimation phone case consumables, you naturally want to purchase items that offer real value for money and boast a high cost-performance ratio, balancing quality assurance with prudent cost control. This article focuses on an industry-leading supplier and manufacturer—Prosub—and systematically deconstructs the logic behind procurement screening. Tailored to diverse needs such as bulk purchasing, small-batch trial production, and premium customization, it provides practitioners with a selection guide to help efficiently match high-quality partners and precisely resolve procurement decision challenges.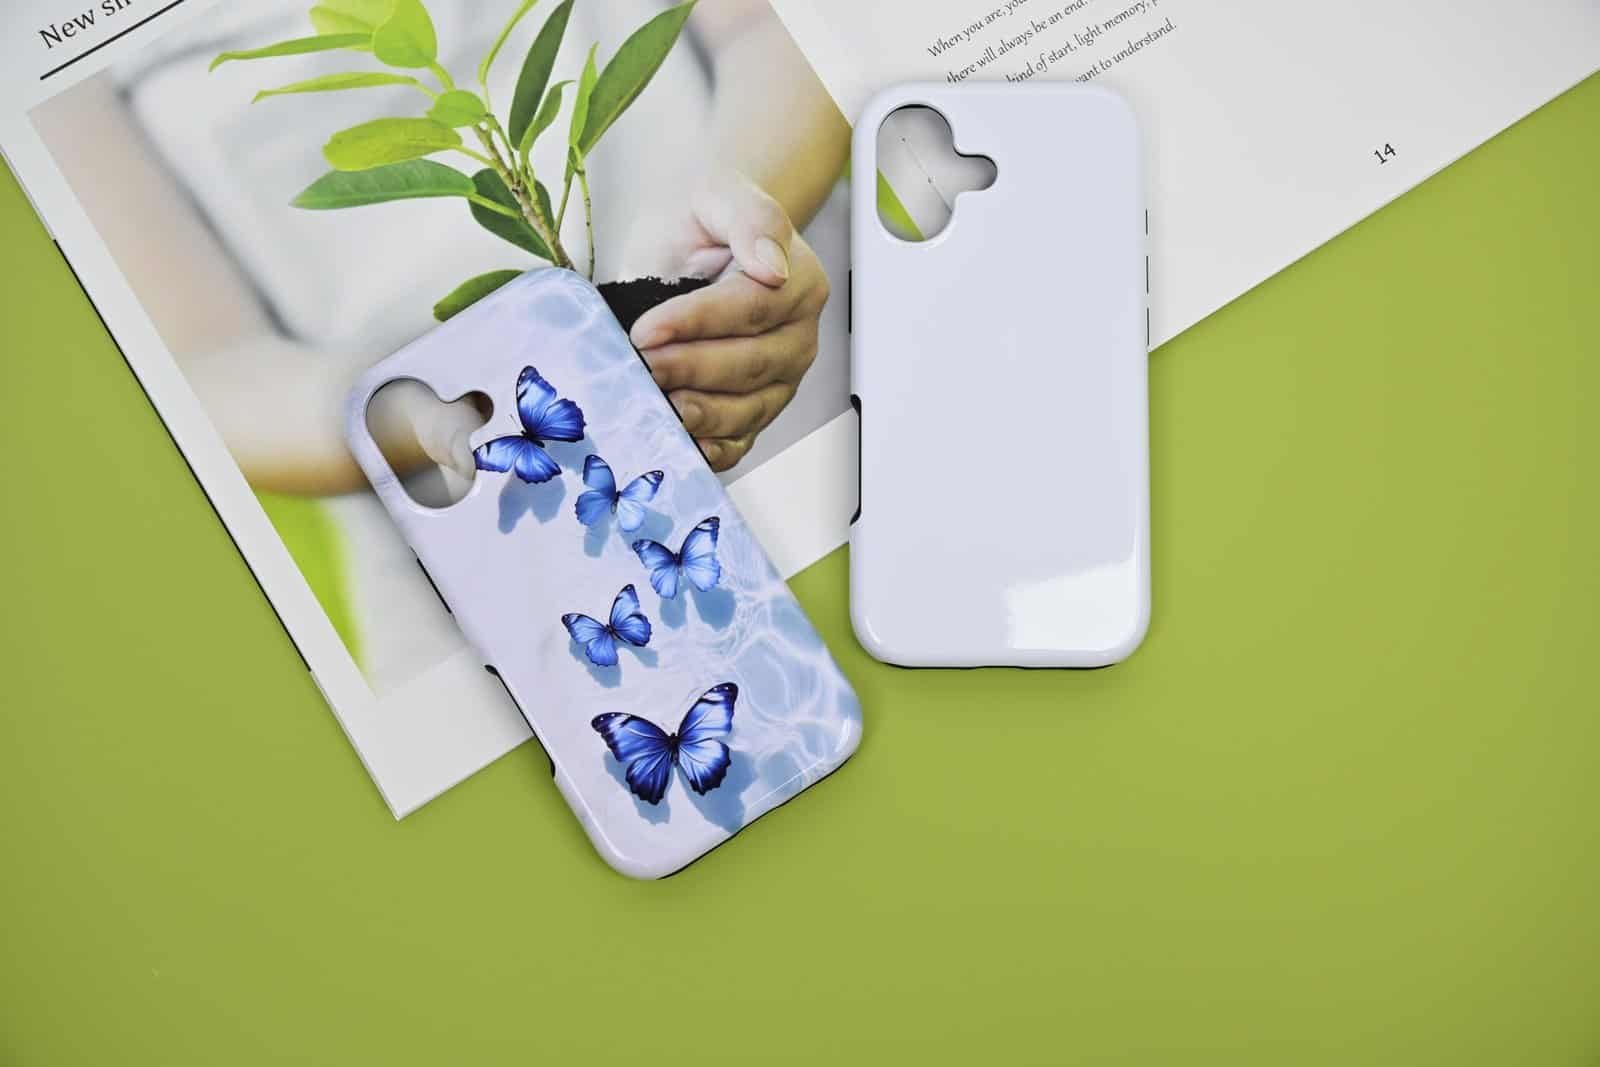
What Are Blank Consumables for Sublimation Phone Cases?
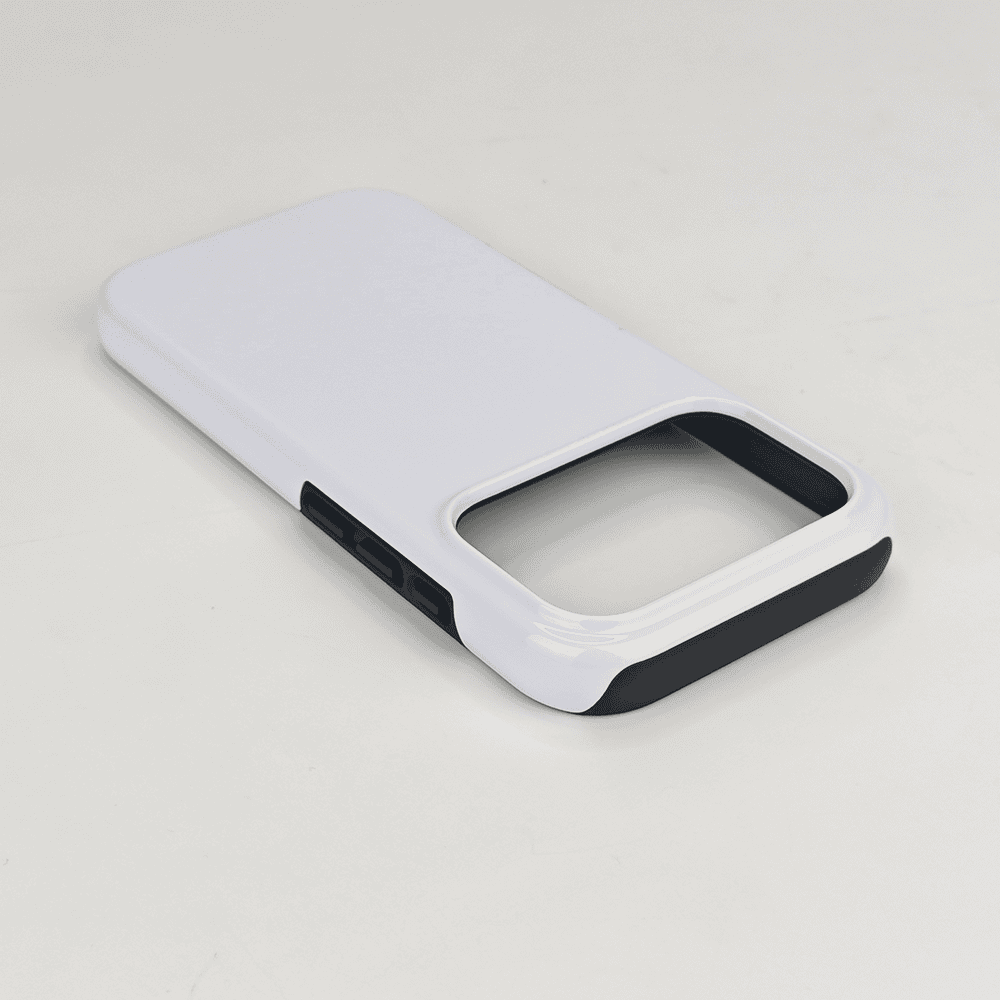
Sublimation phone case blanks are unprinted base substrates designed specifically for do-it-yourself (DIY) personalized designs and intended exclusively for dye-sublimation printing process. Common materials include TPU and PC, with surfaces coated with a special layer formulated to be compatible with sublimation ink. Through sublimation technology, patterns are transferred onto the case surface, resulting in vibrant colors that remain vivid and durable over time.
Key Considerations When Selecting Suppliers of Blank Consumables for Sublimation Phone Cases
Supply Chain Capability
The essence of supply chain capability lies in delivery stability. It is essential to assess whether the supplier maintains sufficient inventory reserves to handle urgent orders, confirm that lead times for both standard and customized orders align with your production schedule, and verify their rapid replenishment capacity during peak periods such as cross-border mega sales events and holiday customization surges, so as to avoid stock-outs.
Product Quality
Product quality is the core competitive strength and determines the service life of the phone cases. Priority should be given to checking the purity, toughness, and flatness of the blank substrate, identifying defects such as deformation or burrs; verifying the uniformity, adhesion, and color fidelity of the sublimation coating, and confirming compatibility with high-resolution printing; and reviewing the supplier’s factory inspection procedures to ensure defect rates remain within the industry-accepted threshold of ≤1%.
Balancing Cost-Performance & Risk Management in Cooperation
Collaboration must strike a balance between cost and risk. Focus on pricing mechanisms, payment terms, and after-sales policies—clarify minimum order quantities (MOQs), tiered discounts, flexible credit periods, and rules for returns/exchanges of defective goods. Also confirm whether they can supply blanks for both mainstream and niche phone models; and whether they support blank customization options such as thickness, shape, and coating type (e.g., matte, glossy), enabling you to create truly unique, personalized phone case designs.
Key Considerations When Selecting Manufacturers of Blank Consumables for Sublimation Phone Cases
Production Strength: Ensuring Scalability and Customization Capability
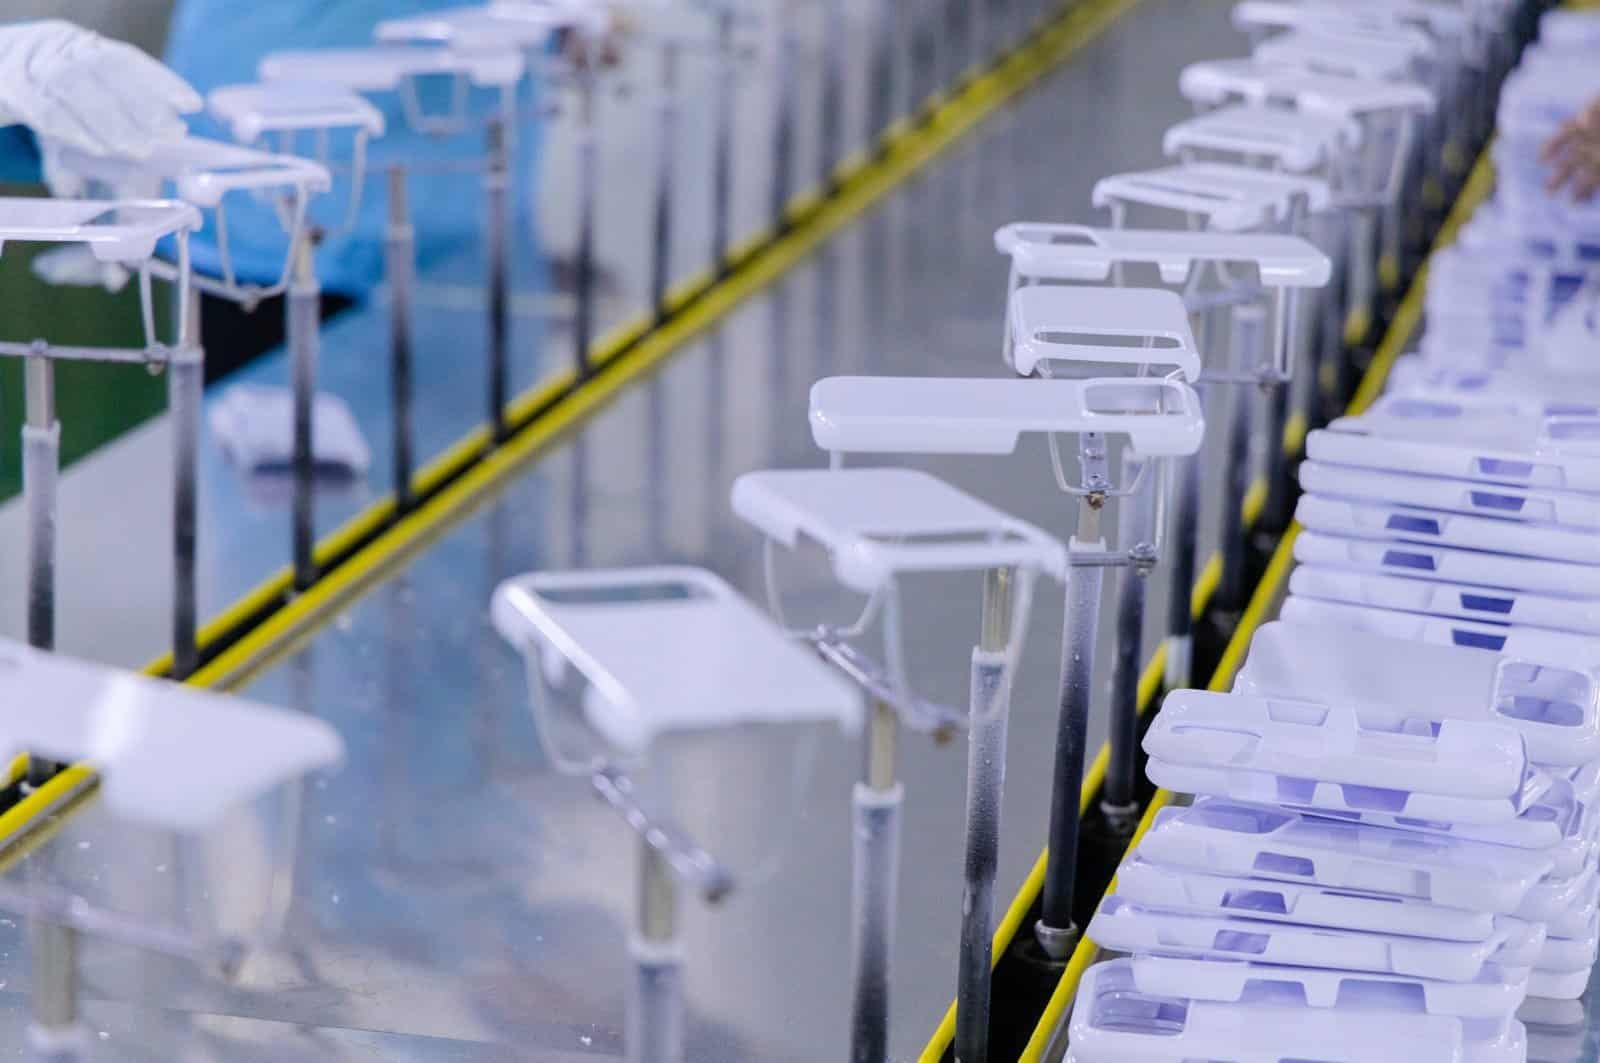
Production scale is the core metric for assessing a manufacturer’s supply capacity. It is necessary to examine factors such as factory floor area, production line configuration, and monthly output to gauge their ability to handle large-volume orders and meet peak-season demand. Advanced automated injection molding and coating equipment are vital to product quality, as they ensure consistency and reduce defect rates. It is also important to evaluate the team’s R&D capabilities, to confirm they can iterate coating formulations and adapt to new phone models, thereby helping create differentiated products. Furthermore, reputable manufacturers typically have richer experience, which often translates into higher product quality.
Qualifications & Compliance: Mitigating Cooperation Risks
Verify the manufacturer’s core qualifications, ensuring they hold a production license, that their coating materials comply with relevant environmental standards and possess eco-certifications, and that their products have passed authoritative quality inspections. At the same time, assess whether their production processes meet environmental compliance requirements to avoid suspension of operations or supply disruptions due to ecological violations. It is also essential to confirm they own patents related to coatings and processes, thereby eliminating potential infringement risks.
Quality Control System: Ensuring Product Quality from the Source
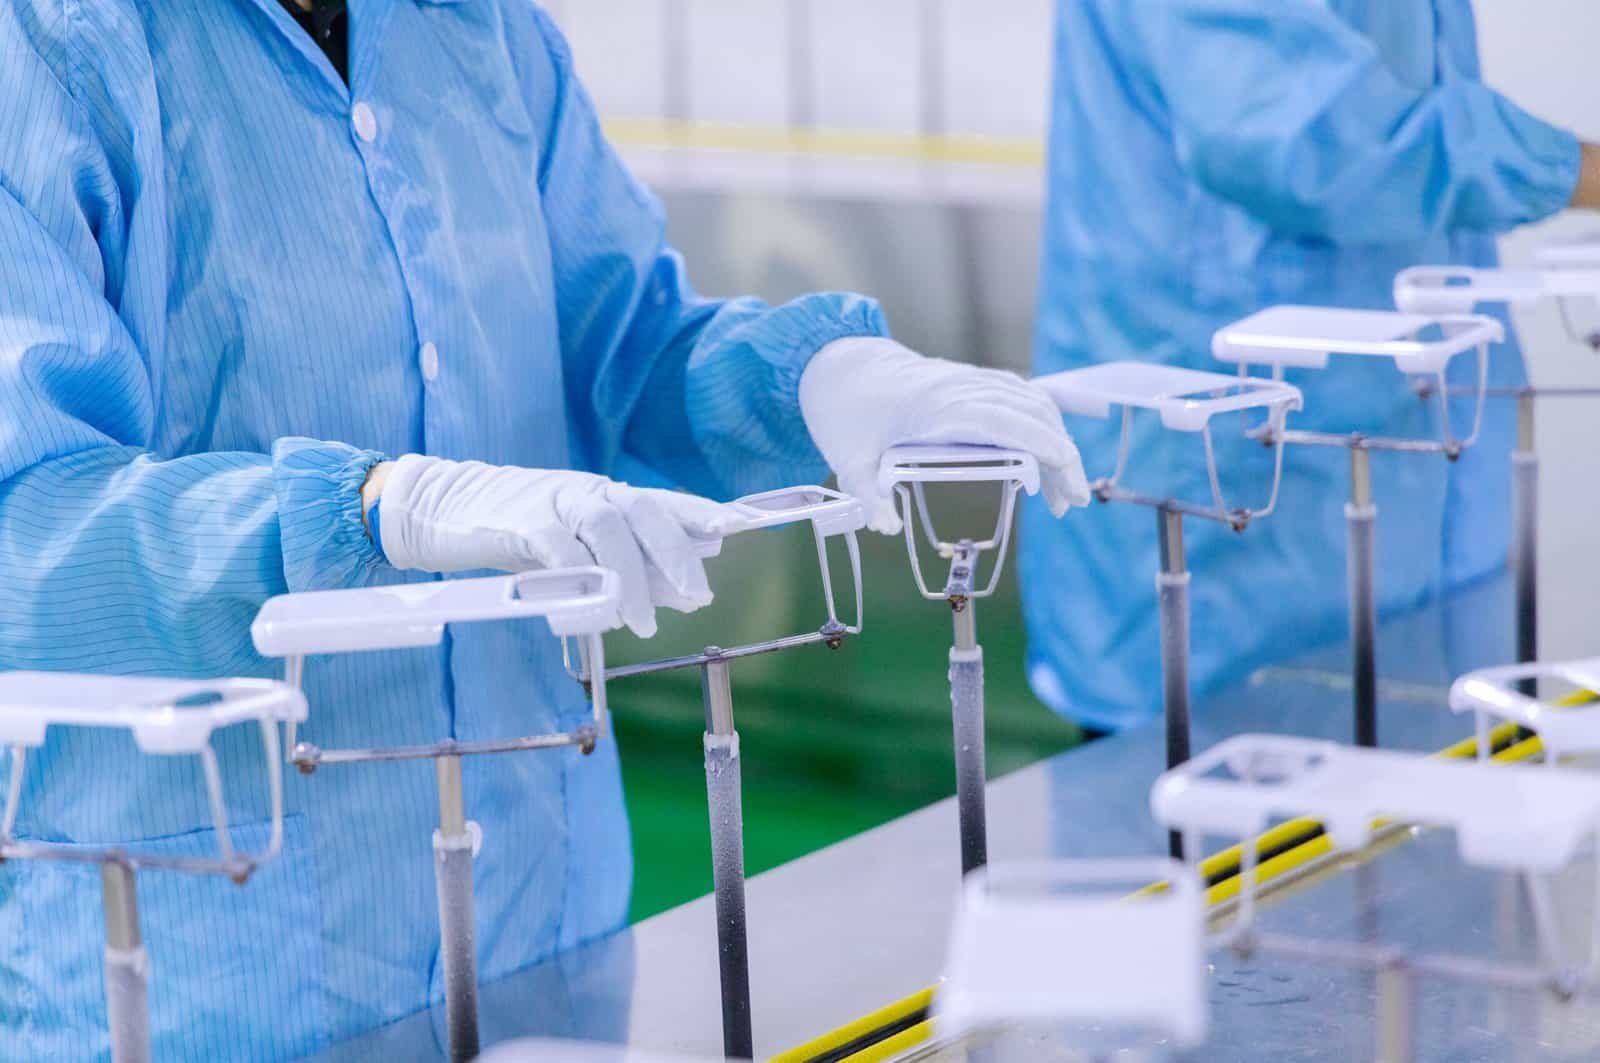
Evaluate the manufacturer’s quality control (QC) system, confirming whether they have established strict standards covering the entire workflow—from raw material procurement, injection molding, coating treatment, to final product inspection. Check if they have batch-level traceability capability for product quality, enabling swift identification of issues. Also consider whether they provide free samples, and whether there is consistency in quality between samples and mass-produced goods.
Consumables Compatibility & Supporting Services: Safeguarding Production Compatibility and Consistency
Before purchasing, be sure to confirm that your sublimation ink is fully compatible with the sublimation blank consumables, and that color fidelity is sufficiently high to guarantee a perfect match in the final product. Consider whether the manufacturer offers related supporting products (e.g., sublimation transfer film, phone case sublimation transfer machines, etc.). Sourcing these from a single supplier helps ensure better compatibility and consistency across products.
Top 10 Suppliers & Manufacturers of Blank Consumables for Sublimation Phone Cases
1,Johnson Plastics Plus
Overview:A leading materials supplier in the United States with over 30 years of history. They offer a wide range of phone case blanks, renowned for their high‑quality coating that ensures accurate color reproduction and long‑lasting durability.
Features:In addition to consumables, they provide professional sublimation transfer paper and technical support.
2,BestSub
Overview:One of the world’s largest manufacturers of sublimation products, headquartered in China, with a global service network.
Features:An extremely extensive product line (over 8,000 SKUs), including 2D and 3D phone cases, as well as various specialized molds.
3,Coastal Business Supplies
Overview:A long‑established one‑stop sublimation supplier, favored by small studios for its “new product bundles” and same‑day shipping service.
Features:Offers rubber, plastic, and flip‑style fabric phone cases for various iPhone and Samsung models.
4,Conde Systems
Overview:A pioneer in the sublimation industry, focusing on professional‑grade custom solutions.
Features:Their phone case blanks are known for stable coating and scratch‑resistant performance, often supplied in bulk to commercial print shops.
5,Heat Press Nation
Overview:Although best known for heat press machines, their SubliCraft series of blanks has grown rapidly in recent years.
Features:As a top‑rated vendor, their phone case kits are ideal for beginners and mid‑size businesses, with exceptionally fast logistics.
6,INNOSUB USA
Overview:Based in Los Angeles, specializing in sublimation accessories for 3C digital products.
Features:Provides custom sizing for large orders and is among the first to supply blanks for the latest iPhone and Samsung models (e.g., mainstream models of 2026).
7,Unisub
Overview:A globally recognized premium brand for hard‑surface sublimation materials, whose products are frequently resold by major distributors.
Features:Uses high‑quality coatings manufactured in the U.S.; excels in color vibrancy and UV resistance, setting industry benchmarks.
8,JDS Industries
Overview:A large wholesale supplier covering trophies, gifts, and personalized décor.
Features:Boasts an extensive warehousing network; phone case blanks span from entry‑level to high‑end business styles.
9,Shenzhen Tuoli
Overview:An electronics technology manufacturer based in Shenzhen, specializing in protective cases for smart devices and related printing equipment.
Features:Offers innovative designs such as 2D aluminum insert card cases and 3D magnetic cases, with rapid prototyping for 2026 new models (e.g., iPhone 17 series).
10,ProSub
Overview:Prosub is a globally leading supplier of sublimation phone case blanks. With 14 years of expertise and patented technologies in sublimation transfer film, blank consumables, and equipment, we provide complete high‑performance solutions for renowned global brands. The company operates two production bases covering more than 33,000 m², exporting to over 80 countries and regions worldwide.
Features: The company has obtained ISO 9001, BSCI, CE, and FCC certifications. Leveraging advanced coating technology as its core, it produces sublimation products that deliver brilliant colors, long-lasting durability, and full compliance with environmental requirements—precisely meeting the high-quality procurement needs of professional creators and enterprise clients. Each production batch is assigned a unique code and archived, enabling full traceability throughout the process. The company holds a technological edge in 3D vacuum sublimation, allowing seamless printing that wraps the entire phone case (including side edges and corners).
Advantages:Prosub offers an end-to-end, one-stop sublimation phone case solution covering the entire workflow from design to delivery — including blank consumables, sublimation equipment, sublimation film, and more. Moreover, there is no minimum order quantity (MOQ) for our products, and we provide comprehensive OEM/ODM customization services along with one-stop technical guidance to help clients successfully bring their custom products to market.
Conclusion
Selecting high-quality sublimation phone case blank hinges on the precise alignment of quality, supply capability, and service. With 14 years of deep industry experience, full-chain quality control, and robust customization capabilities, Prosub delivers highly adaptable solutions to clients worldwide. We aim to be your reliable partner for all sublimation printing needs.